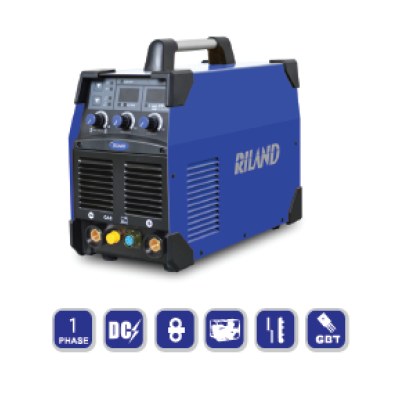
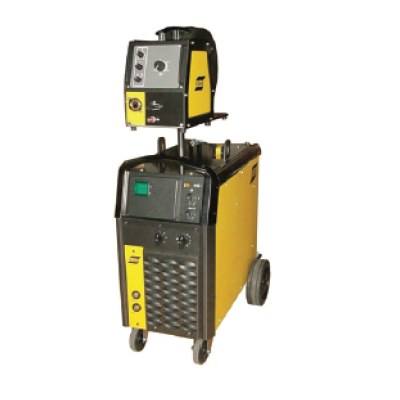
Description: MIG 251 GF is a powerful, reliable and compact equipment for any light to medium welding using MIG or Flux cored wire. It is light weight and easily movable.…
Features: MIG; MMA; Inverter power source; MIG torch; Earth clamp; Hose; Hose clamp; Adjustable current, voltage and inductance
Request for QuotationThis item is quoted on request (imported / made to order). Send the quantity and we reply with the price in PKR, delivery time and any bulk discount.
MIG 251 GF is a powerful, reliable and compact equipment for any light to medium welding using MIG or Flux cored wire. It is light weight and easily movable. Built in IGBT invertor technology this machine is an economical choice for the industry, maintaining its reliability for MIG and MMA applications.
Features
MIG; MMA; Inverter power source; MIG torch; Earth clamp; Hose; Hose clamp; Adjustable current, voltage and inductance
Input Power
220V/7.92KVA/ 1P/50-60Hz
Amps Input at Rated Output
MIG: 36A@200A MMA: 32A@160A
Output Range/OCV
MIG: 50-200A/56V MMA:40-160A/56V
Dimension ( mm )
468*245*478
Weight ( Kg )
15.4
IP Class
IP21
Insulation class
F
Supply
sizes, packing and price confirmed with your quotation
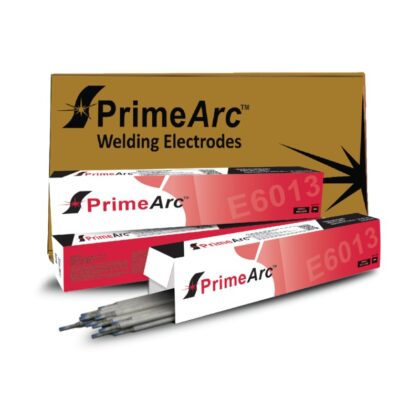
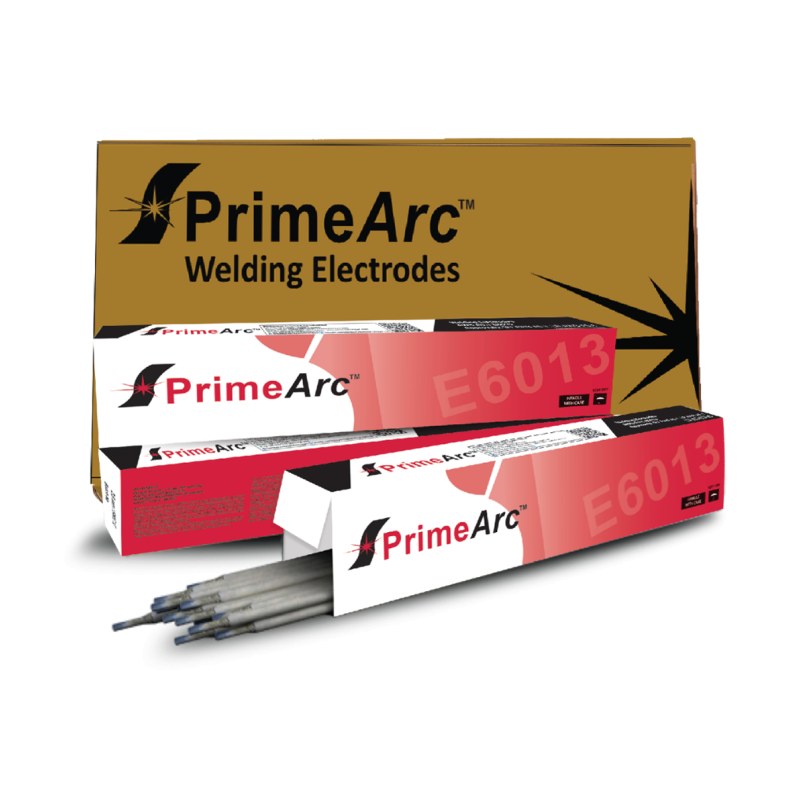
Prime. Arc™ E6013 is a mild steel welding electrode coated with rutile, suitable for both AC or DC that delivers outstanding welding performance. It is engineered for low-carbon steel applications, delivering high-quality welds, excellent deposition rates, and stable arc performance. It is also perfect for cosmetic welding that demands an optimal bead appearance and smooth surface.
Size (mm)
2.5 x 300, 3.2 x 350, 4.0 x 400, 5.0 x 400
Current (amps)
60-90, 80-130, 150-190, 180-25
Tensile strength (N/mm2)
386
Yield strength (N/mm2) minimum
464
Elongation (%) minimum
24
Charpy V impact values at 00C minimum
>47
Type of Current
AC, DCEP or DCEN
Type of covering
Rutile-cellulosic electrode
Classification
AWS A/SFA 5.1-91 E6013; EN 499 E 38 0 RC 11; EN ISO 2560-A E 38 0 RC 11
Approvals
BV, LR
Supply
sizes, packing and price confirmed with your quotation
MIG; TIG; FCAW; MMA; Multi-Process including MIG, Flux-Cored, Stick, Live TIG and Arc Gouging gives you the flexibility at work: Flux - Cored and Solid wire, 0.8 -1.6 mm, Carbon Arc Gouging up to 9.5 mm (3/8 in) - 6010 (cellulosic) capability; Outstanding welding characteristics - high efficiency and quality welding; Standard digital V/A meter kit – makes parameters visible and helps to improve weld quality; Sturdy galvanised metal casing with air filter as option - made to withstand tough corrosive and adverse environments
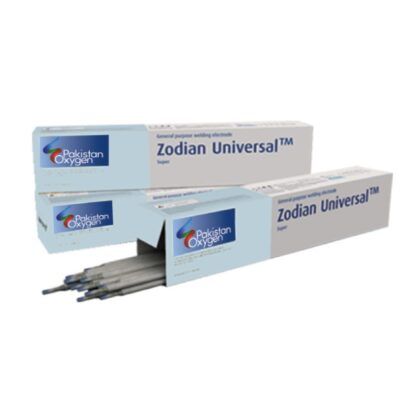
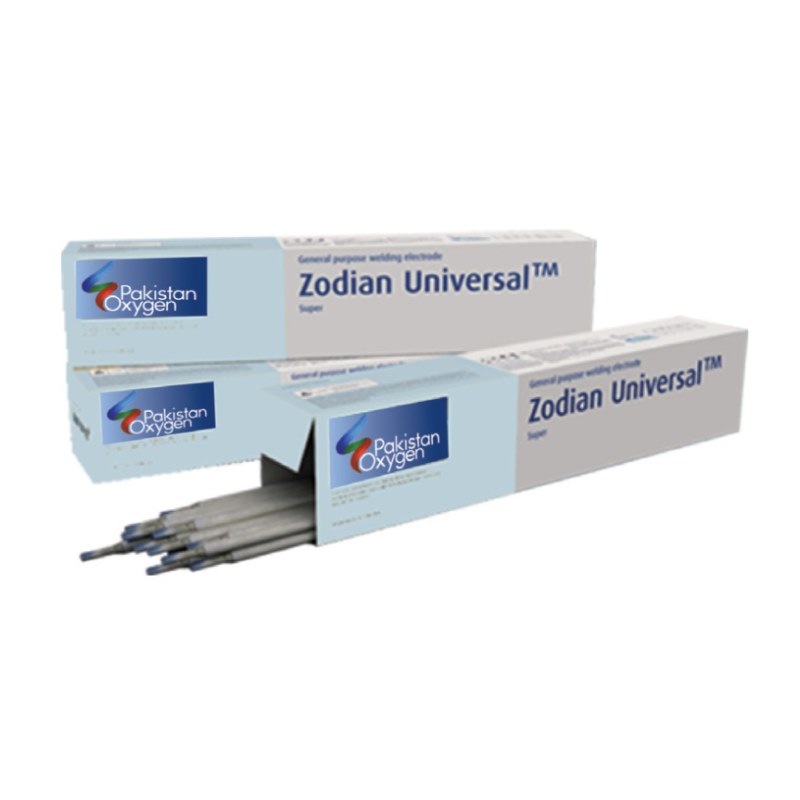
Zodian Universal E6013 is a rutile-coated, general-purpose, mild steel/carbon steel, welding electrode. It has high arc force, good penetration and easy slag detachability resulting in quality welding joints even on rusty plates and uneven surfaces. It is suitable for all-positional welding and is particularly suited for downward, horizontal and vertical conditions.
Size (mm)
2.5 x 305, 3.25 x 350, 4.0 x 350, 5.0 x 350
Current (amps)
75-90, 90-120, 130-190, 180-230
Tensile strength (N/mm2)
470-600
Yield strength (N/mm2) minimum
380
Elongation (%) minimum
24
Charpy V impact values at 00C minimum
47 (Joules)
Type of Current
AC, DCEP or DCEN
Type of covering
Rutile-cellulosic electrode
Classification
AWS A/SFA 5.1-91 E6013; EN 499 E 38 0 RC 11; EN ISO 2560-A E 38 0 RC 11
Approvals
LR
Supply
sizes, packing and price confirmed with your quotation
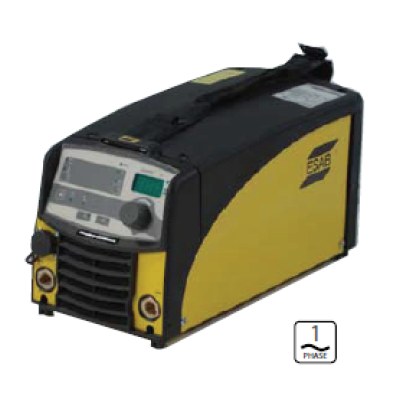
MMA; TIG; Adjustable hot start easy to strike the electrode. Helps you to avoid starting problems; Adjustable arc force sets the intensity of the arc for improved weld quality; Better welding characteristics, simplifies your work and gives you better weld quality with less after treatment; Extra long mains cable capability gives extra large working radius
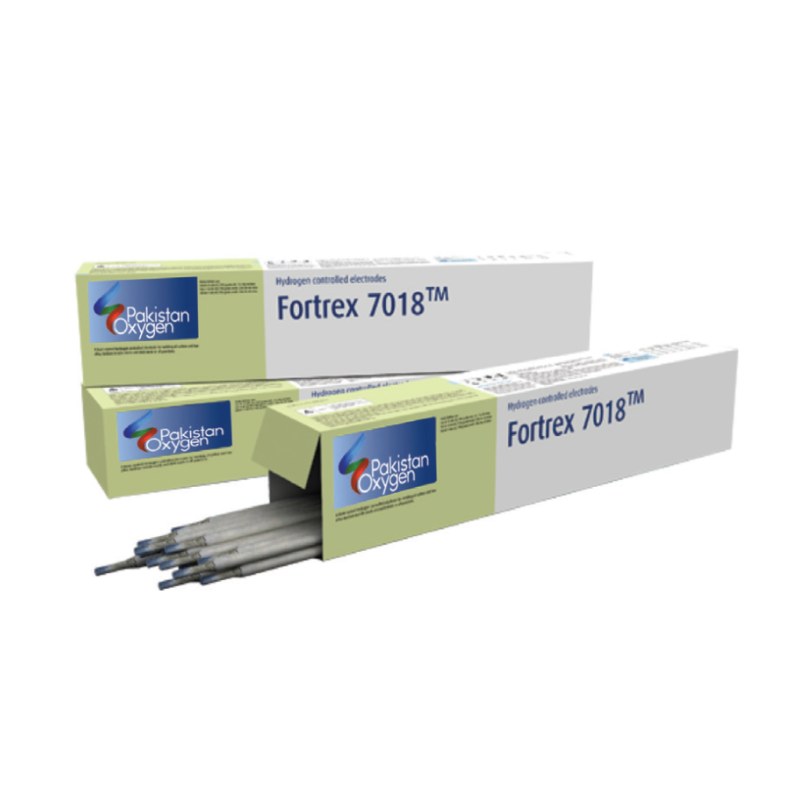
Fortrex 7018 is a basic-coated hydrogen controlled electrode designed for all-positional (except vertical-down) welding of carbon, alloy and strong tensile strength steels, and of mild steels under conditions of high restraint. It has high arc force, good penetration and easy slag detachability resulting in supreme quality welding joints even on rusty plates and uneven surfaces.
Size (mm)
2.5 x 305, 3.25 x 400, 4.0 x 400, 5.0 x 400
Current (amps)
75-90, 90-130, 120-180, 160-220
Tensile strength (N/mm2)
510-640
Yield strength (N/mm2) minimum
410
Elongation (%)
22
Charpy V impact values at -20 C minimum
162 (Joules)
Type of Current
AC, DCEP or DCEN
Type of covering
Basic-coated, Hydrogen controlled
Classification
AWS A/SFA 5.1-91 E7018; EN 499 E 42 3 B 32 H5; EN ISO 2560-A E 42 3 B 32 H5
Approvals
ABS, LR
Supply
sizes, packing and price confirmed with your quotation

Reviews
There are no reviews yet.